BESS Quality Assessment Checklist: Cells, FAT, Shipment and Site Acceptance
A BESS quality assessment checklist helps buyers confirm that a battery energy storage system is built, tested, shipped and installed as specified, rather than judging quality from a brochure or a single factory visit. Quality problems in a commercial and industrial (C&I) battery energy storage system rarely come from one dramatic defect. They usually come from small gaps: an unapproved component substitution, a cell batch that was not matched, a loose connection missed during assembly, a firmware version that differs from the tested one or packaging damage that nobody recorded.
This guide is written for C&I energy storage buyers, EPC contractors, distributors and project owners. It organizes quality assessment into gates across the whole project life, from cell supply to early operation. It does not set universal acceptance limits. The supplier’s approved specifications, the purchase contract, applicable standards and local requirements remain the controlling documents. Use the checklist to decide what evidence to request at each stage and who should review it.
What a BESS quality assessment should prove
A quality assessment should answer three questions. First, does the delivered system match the approved design, including components, configuration, firmware and documents? Second, has each stage been checked against written criteria, with results that can be traced to serial numbers? Third, are nonconformances closed or formally accepted before the equipment moves to the next stage?
These questions apply to the whole system, not only the battery cells. A BESS combines cells, modules, racks, the battery management system (BMS), power conversion system (PCS), energy management system (EMS), thermal management, fire detection and suppression interfaces, switchgear, enclosures and software. A strong cell supplier does not guarantee a well-built cabinet, and a clean factory does not guarantee a correct installation.
Set quality gates before the purchase order
Quality assessment is easiest to enforce when the gates are written into the contract. Define the documents the supplier must submit, the inspections the buyer can witness, the tests that must pass before shipment and the records required at handover. State how much notice the supplier must give before each inspection and what happens if a gate is missed.
Start with supplier capability. The C&I ESS supplier qualification checklist helps compare suppliers on factory evidence, PCS scope and warranty support. Then require a project-specific quality plan and inspection and test plan with review, witness and hold points, as described in the C&I ESS manufacturing quality plan guide. The quality plan becomes the reference for every later assessment.
Assess the cell supply before assembly
Cells determine much of the system’s capacity, lifetime and safety behavior. Ask the supplier to identify the cell manufacturer, cell model, chemistry, datasheet revision and production batches planned for the project. If the supplier may use more than one cell source, the contract should state whether substitution requires buyer approval and what evidence must accompany it.
Incoming cell checks
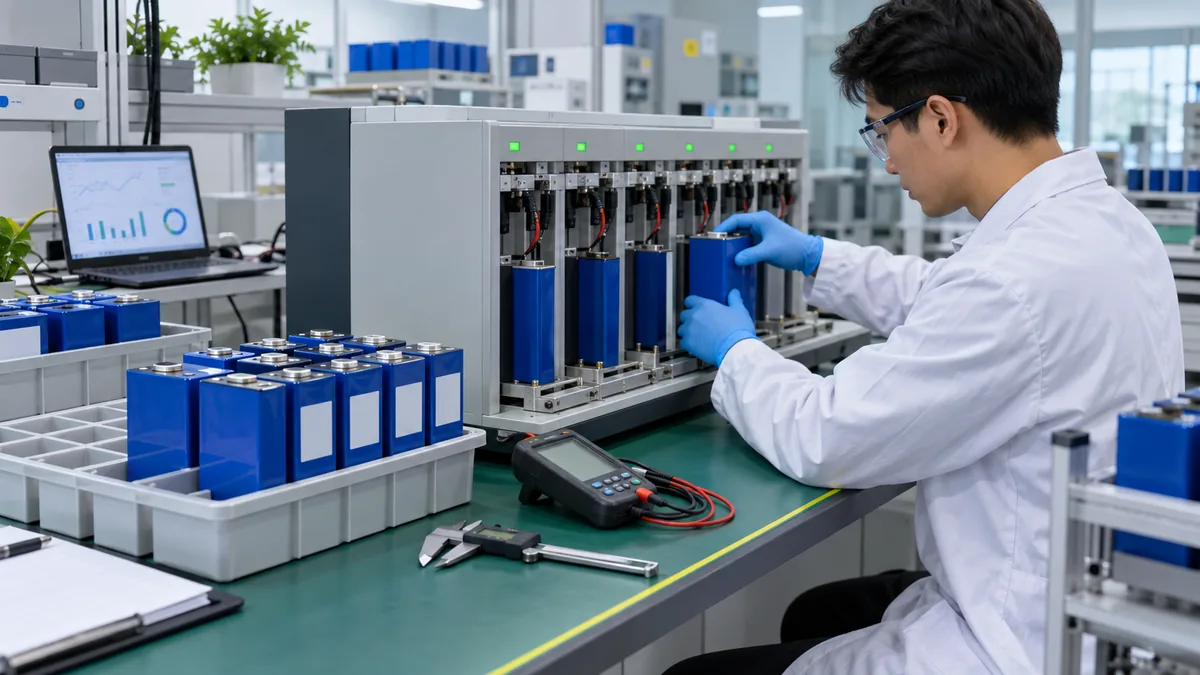
Request the incoming inspection procedure and sample records. Typical checks include appearance, dimensions, terminal condition, open-circuit voltage, internal resistance and batch identification. The records should show the sampling plan, the acceptance criteria and what happened to cells that failed. A summary stating that all cells passed, without the underlying data, is weak evidence.
Cell grading and matching
Cells that are connected in series should be grouped according to the supplier’s matching method, usually based on capacity, voltage and internal resistance. Ask how cells are graded, how long they rest before measurement, which parameters are used for matching and how matched groups are traced into modules. Poor matching can lead to earlier imbalance and reduced usable capacity over time. Also confirm the certification evidence required for the target market, such as cell safety testing to IEC 62619 or system-level listing, and check that the documents refer to the same cell model that will be used.
Check module, rack, BMS and cabinet build
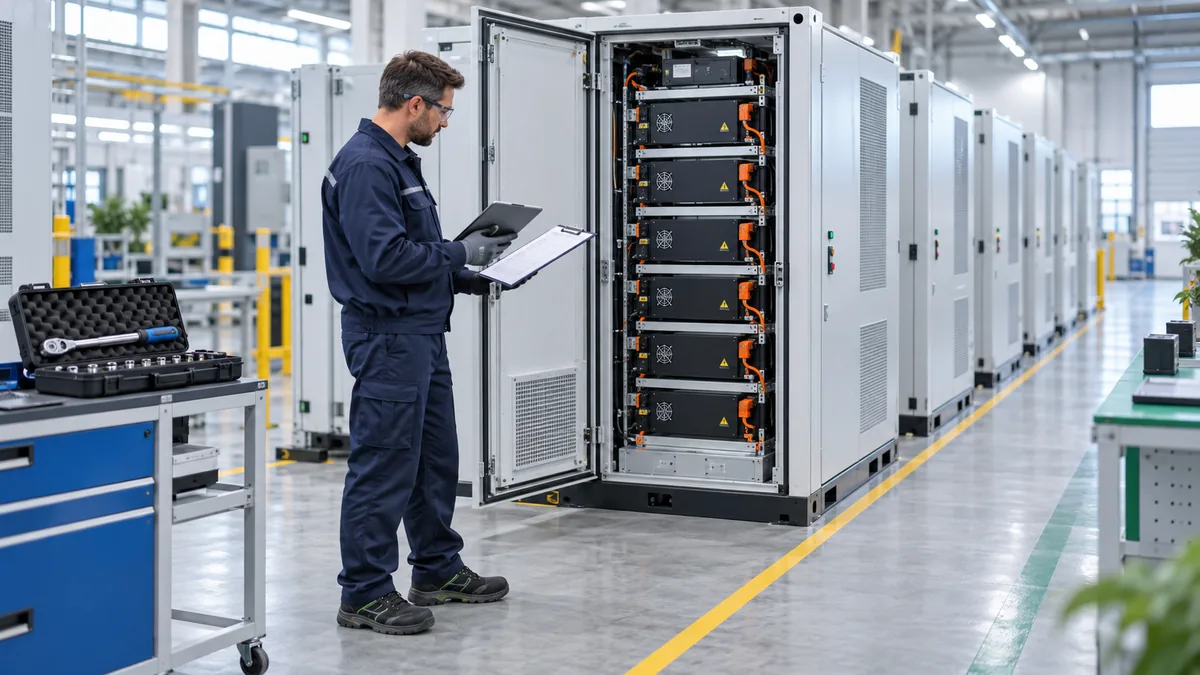
Assembly quality is where many field faults begin. Review the work instructions and records for busbar connections, torque control, cable routing, insulation, labeling, sensor placement and sealing. Torque values should be recorded or marked according to the supplier’s procedure, and critical connections should be checked by a second person or verified with a controlled tool.
Confirm that BMS hardware, firmware and parameter settings match the approved baseline. Protection thresholds, balancing settings and communication settings should be documented and version-controlled. The BMS parameters checklist explains which settings buyers typically review. For the complete cabinet or container, check the PCS, HVAC or liquid cooling, fire detection and suppression interfaces, auxiliary power, grounding and door or access interlocks. The C&I ESS factory audit checklist covers what to look for during a factory visit.
Use FAT to test the delivered configuration
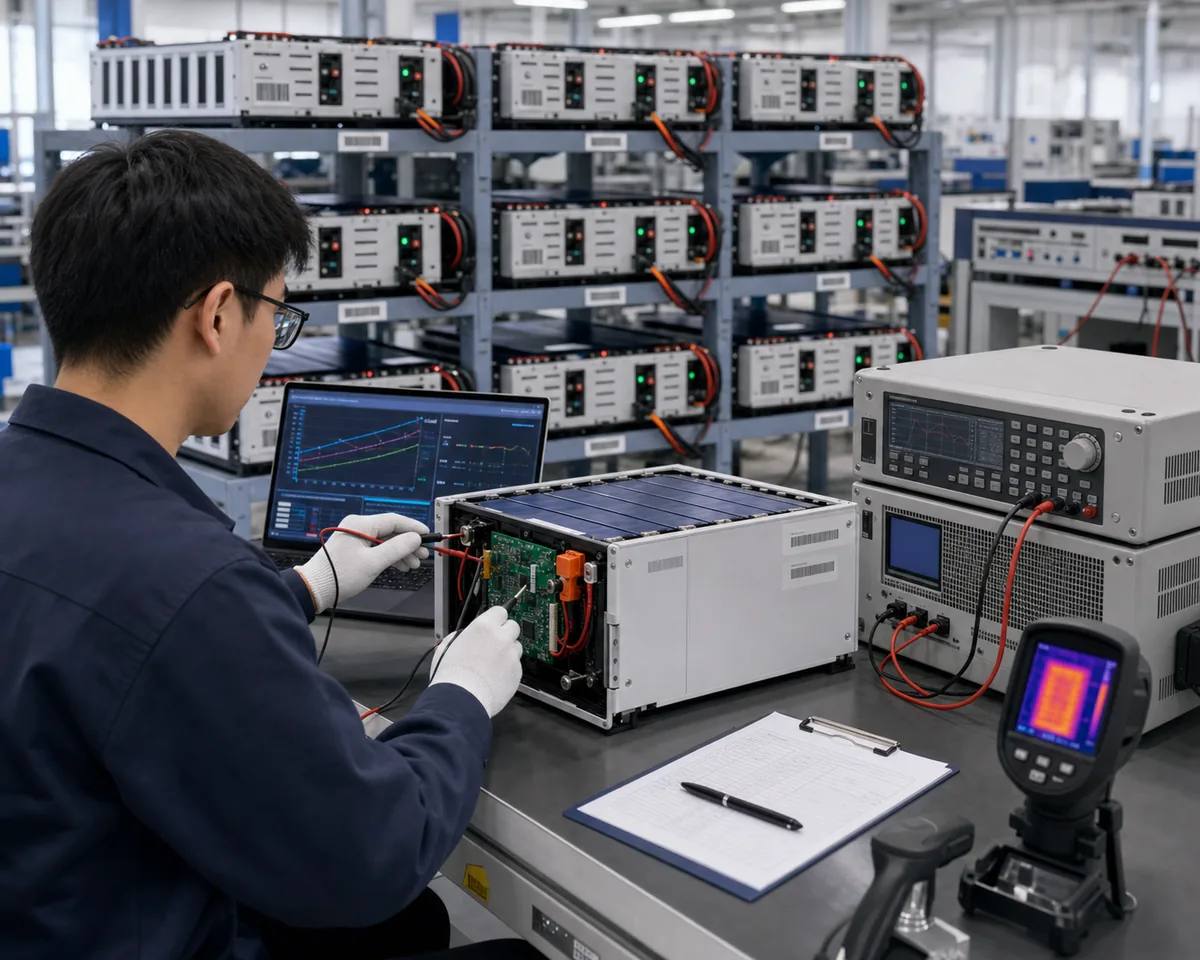
A factory acceptance test (FAT) should test the equipment that will be shipped, in the configuration that will be installed. Agree the FAT procedure in advance, including functional tests, protection tests, communication tests, insulation checks, charge and discharge tests within the approved limits and alarm verification. Record firmware versions and settings during the test, and require that any later change be documented and justified.
Keep raw data, not only the final report. Charge and discharge curves, alarm logs, insulation readings and communication tests are more useful than a signed summary when a question arises later. For battery-level FAT considerations, the LiFePO4 battery factory acceptance test guide lists records OEM buyers should review.
Inspect packing before shipment release
A system that passed FAT can still arrive damaged. Before release, confirm the state of charge required for transport, the securing of internal components, moisture protection, shock and tilt indicators where used, labeling and the packing list. Photograph each packed unit with its serial number, and record the container loading position, blocking and bracing, and seal number.
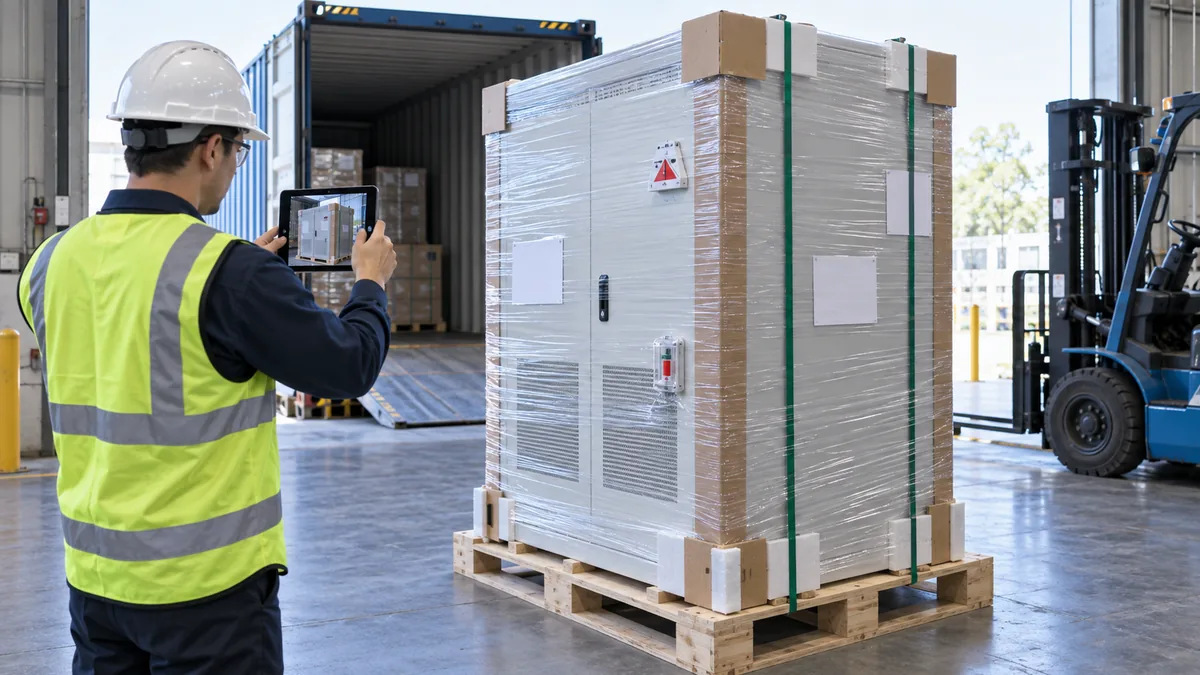
Shipment release should also confirm that transport and import documents are complete and match the delivered equipment. Lithium batteries are regulated as dangerous goods in transport, so missing or mismatched documents can delay a shipment even when the equipment is in good condition. The C&I ESS import documentation checklist covers UN38.3 evidence, safety data sheets and customs files.
Verify condition on arrival
Receiving inspection is the buyer’s first chance to document transport damage before responsibility becomes unclear. Inspect the container seal, the loading condition, packaging, indicators, visible damage, moisture and quantities before unloading is complete. Report damage promptly according to the shipping and insurance terms, and keep the damaged packaging and photos until the claim is settled.
Receiving inspection records
Record the date, inspector, container and seal numbers, serial numbers received, packaging condition, indicator status and any exceptions. Store battery equipment according to the supplier’s instructions while it waits for installation, including temperature, humidity, weather protection and state-of-charge limits. Long storage periods may require periodic checks, and the supplier should state what is needed to keep the warranty valid.
Confirm performance at site acceptance
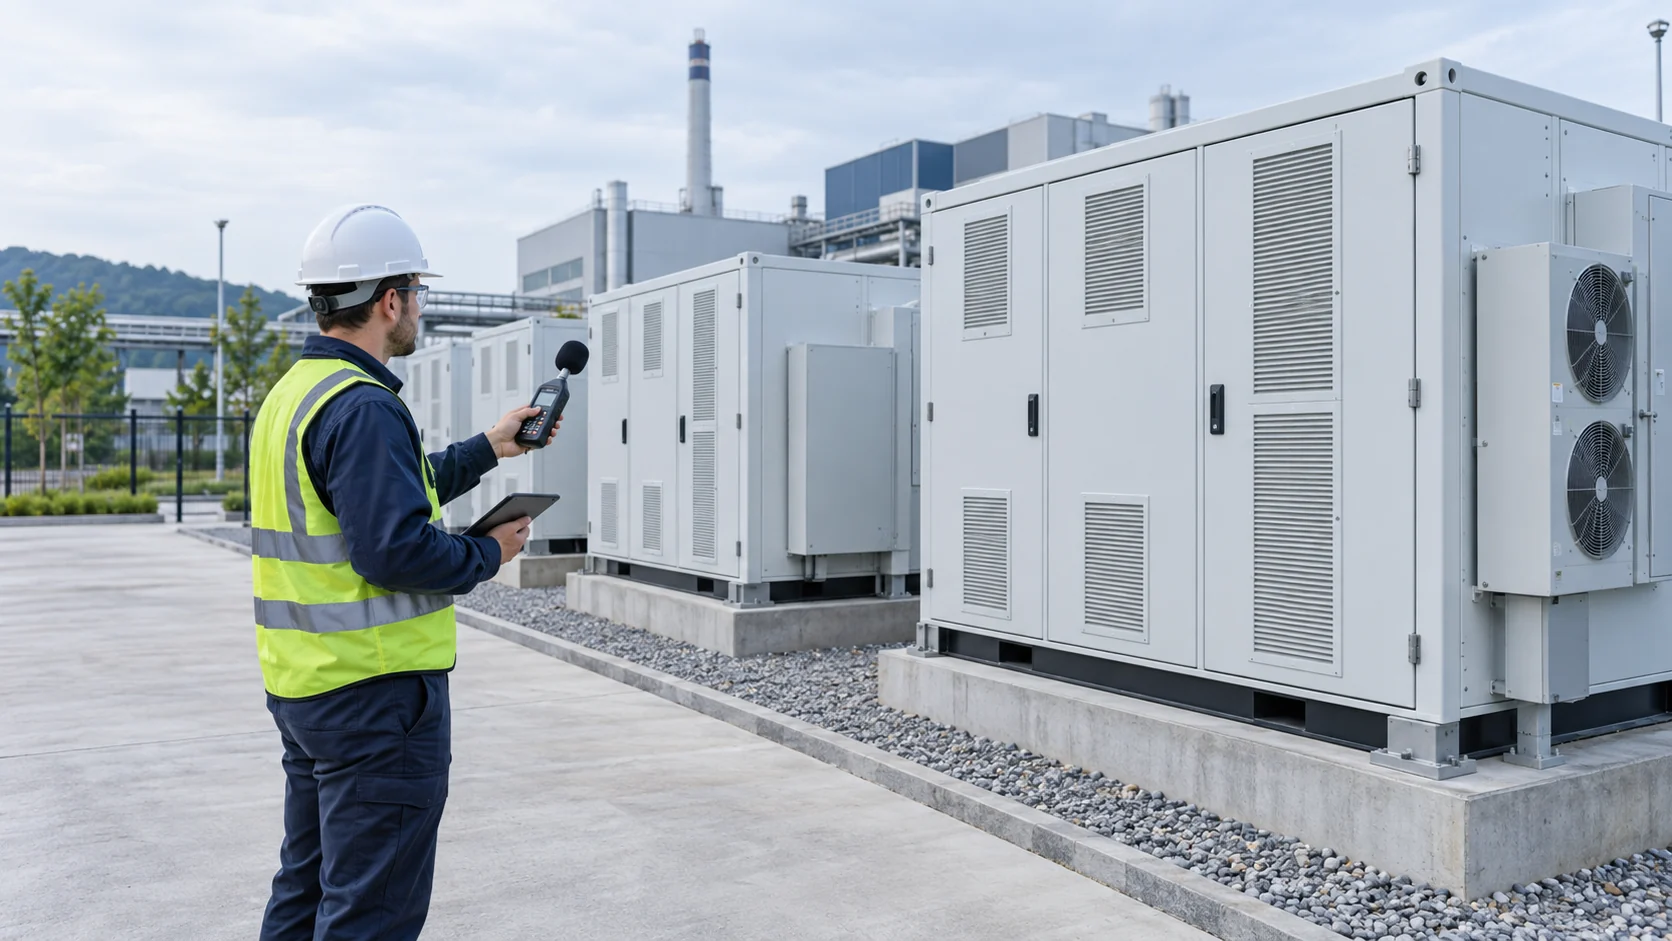
Installation quality is part of system quality. Before energization, check foundations, anchoring, clearances, cable terminations, grounding, labeling, fire-system interfaces and ventilation paths against the approved drawings. Verify that the installed firmware and settings match the FAT baseline or document any approved changes.
The site acceptance test (SAT) should repeat key FAT checks under real site conditions and add grid, metering and control tests. Confirm protection functions, emergency stops, communication with the EMS and site meters, alarm reporting and operating modes. The C&I ESS commissioning checklist covers FAT, SAT and handover evidence in more detail, and fire-system documents are covered in the C&I BESS fire safety document checklist.
BESS quality assessment checklist
| Quality gate | What to assess | Evidence to keep | Common gap |
|---|---|---|---|
| Contract | Quality plan, inspection points, notice periods and substitution rules. | Approved quality plan and inspection and test plan. | Gates agreed verbally but not written. |
| Cells | Cell model, batches, incoming checks and matching method. | Incoming records, grading data and certificates. | Certificates for a different cell model. |
| Assembly | Connections, torque control, wiring, sensors and sealing. | Traveler records, torque marks and photos. | Loose or unverified busbar connections. |
| Configuration | BMS, PCS and EMS firmware and parameter baselines. | Version list and configuration backups. | Firmware changed after FAT without notice. |
| FAT | Functional, protection, communication and performance tests. | Raw data, alarm logs and signed report. | Test performed on a different unit. |
| Shipment | Packing, indicators, transport documents and loading. | Photos by serial number and seal record. | No evidence of condition at departure. |
| Site | Receiving condition, installation, SAT and handover. | Receiving report, SAT results and as-built file. | Damage found after responsibility is unclear. |
Track early-life quality after handover
Some quality problems appear only after the system has operated for a while. Recurring alarms, uneven temperatures, growing cell voltage spread or communication dropouts in the first months of operation can indicate assembly, matching or configuration issues. Treat the early operating period as the last quality gate rather than as normal maintenance.
What to review in the first months
Compare operating data with the SAT baseline. Review alarm history, cell and module voltage spread, temperature distribution, balancing activity, available energy and any derating events. Record each issue with its serial number, time and corrective action, and ask the supplier for a root-cause explanation when a problem repeats. The C&I ESS battery degradation monitoring checklist explains how to build a consistent data record for later performance and warranty reviews.
Decide who performs each assessment
Assign every gate to a responsible party. The supplier performs its internal inspections and tests. The buyer or EPC reviews documents and witnesses selected tests. The installer performs installation checks. The owner or its operator reviews early operation. When roles are not written down, each party may assume that another one has checked the evidence.
When independent inspection adds value
An independent inspector can help when the buyer cannot attend the factory, when the project is large or safety-critical, when the supplier is new or when a lender or insurer requires independent evidence. Give the inspector the approved specifications, the quality plan and the checklist for each gate, and ask for photos and raw data rather than a pass or fail statement alone. General research on energy storage safety and reliability is available from Sandia National Laboratories’ energy storage program, and installation requirements in many markets reference NFPA 855 for stationary energy storage systems.
For project equipment options, review the C&I ESS product range, then send the site location, required capacity and quality requirements through the SolarStorageHub contact page for a scope discussion.
FAQ
What is a BESS quality assessment?
It is a structured review of evidence showing that a battery energy storage system was built, tested, shipped and installed according to the approved design, with results traceable to serial numbers.
Is a factory audit enough to assess BESS quality?
No. A factory audit shows the supplier’s capability, but the project still needs cell records, assembly checks, FAT, shipment inspection, receiving checks and site acceptance.
What evidence should a buyer request after FAT?
Request the signed FAT report, raw test data, alarm logs, firmware and settings records, and a list of any open or accepted nonconformances.
When should an independent inspector be used?
Consider an independent inspector when the buyer cannot attend, the project is large or safety-critical, the supplier is new, or a lender or insurer requires independent evidence.
Related SolarStorageHub Resources
If you are turning this article into a buying decision, compare the relevant product families and send your inverter model, target capacity, installation country, and quantity plan for confirmation.